Air Handling Unit
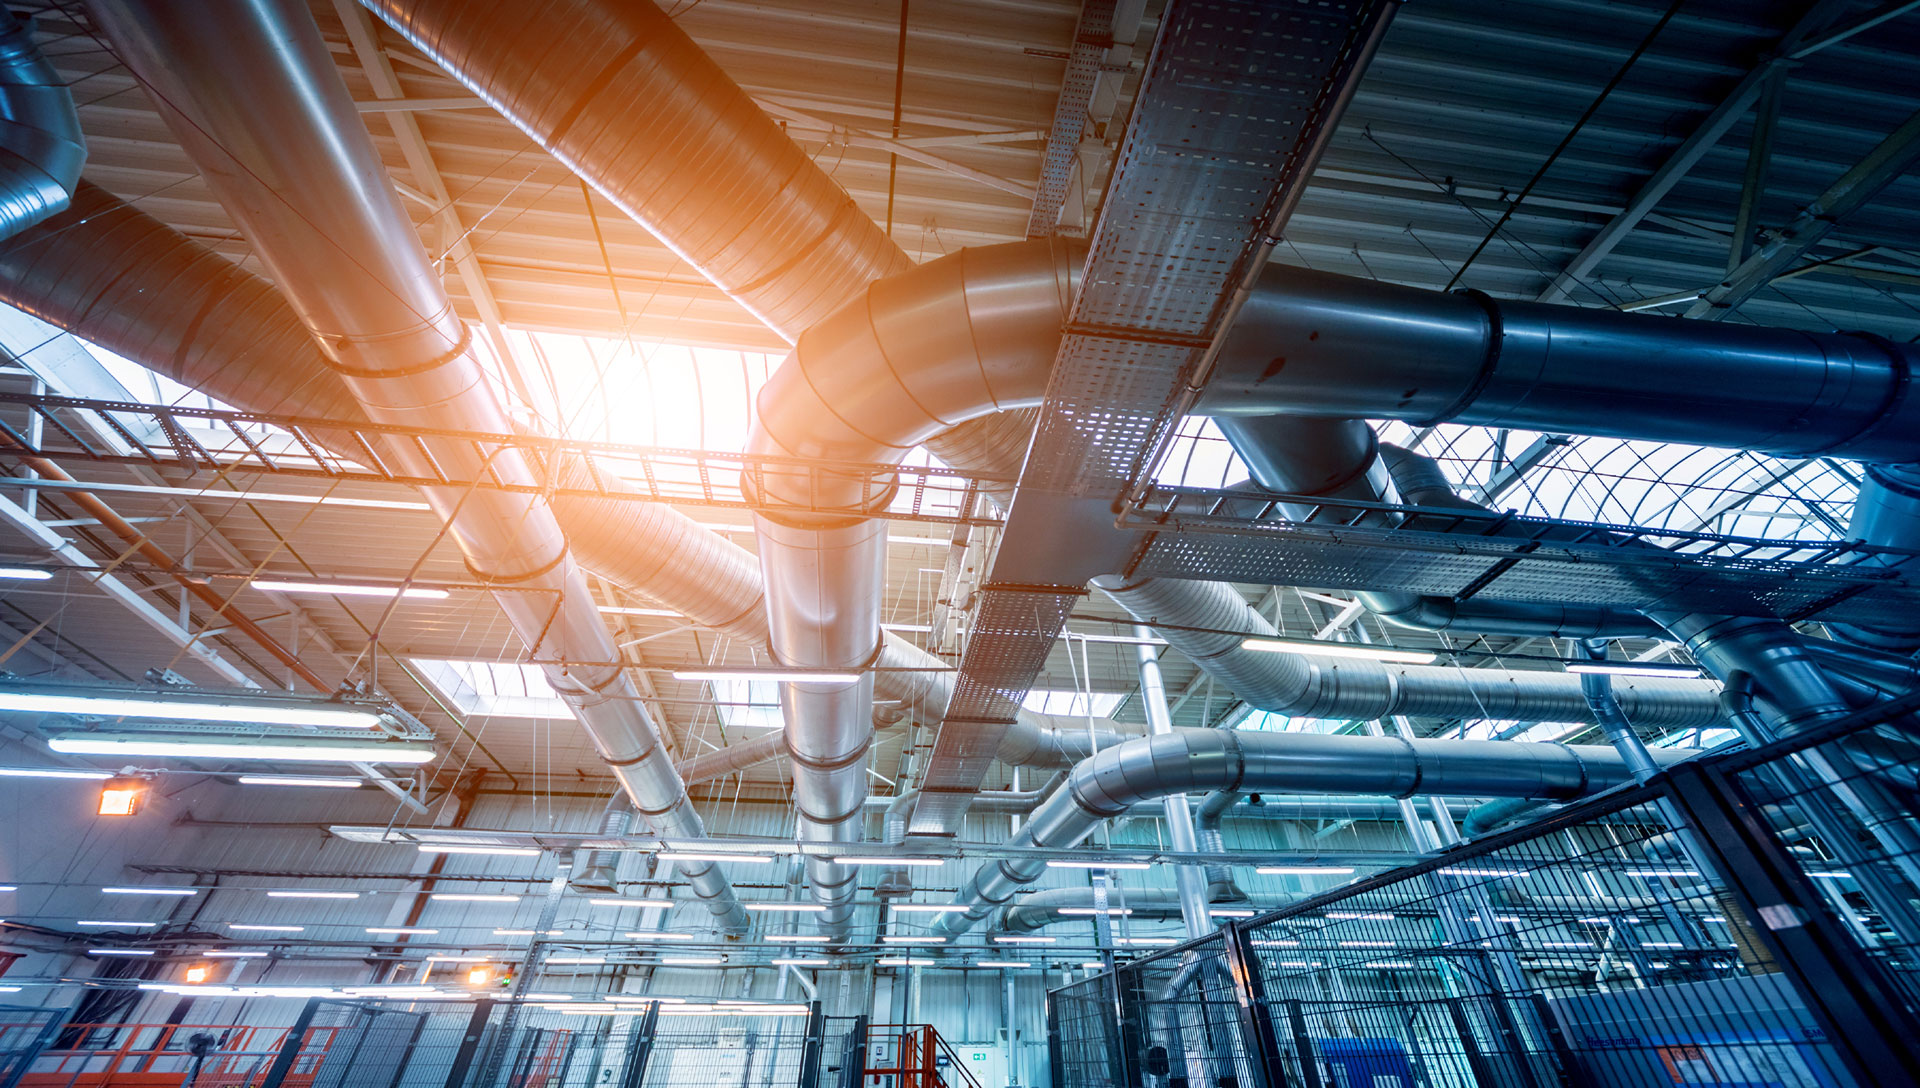
We provide high-quality Air Handling Units (AHUs) for efficient air circulation, temperature control, filtration, and indoor air quality.
Read More
Renowned for our dedication to innovation and customer satisfaction, we’ve become industry leaders by combining advanced technology with high-quality cleanroom solutions. Our tailored services meet the unique needs of every client, delivering reliable, efficient systems. By adapting to evolving market demands, we consistently exceed expectations, build lasting partnerships, and drive success across diverse industries.
Read More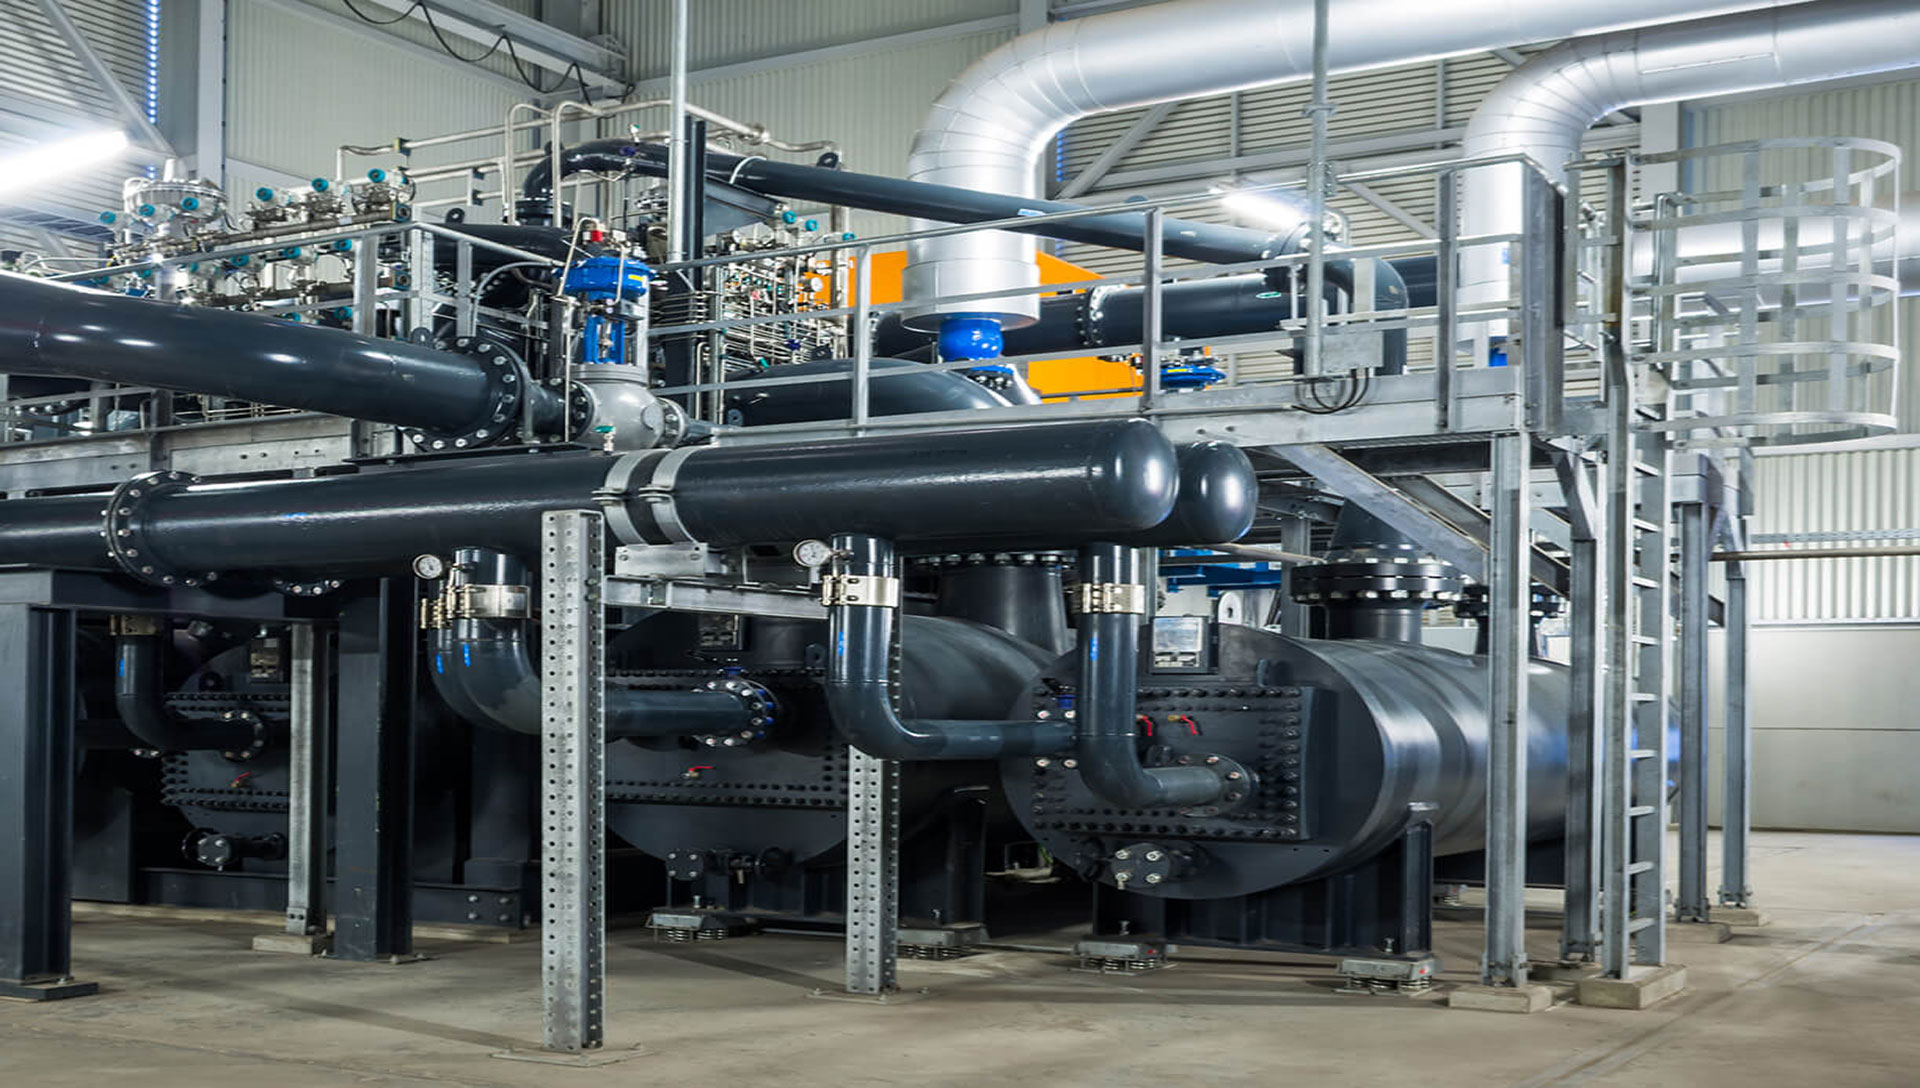
At PKB Projects, we lead in manufacturing, trading, and servicing high-quality cleanroom solutions. With years of experience, we deliver products tailored to pharmaceuticals, biotechnology, healthcare, and research. Our offerings include modular partitions, cleanroom equipment, HVAC systems, and turnkey setups—each engineered to meet the highest standards of performance, hygiene, and compliance in controlled environments.
Read More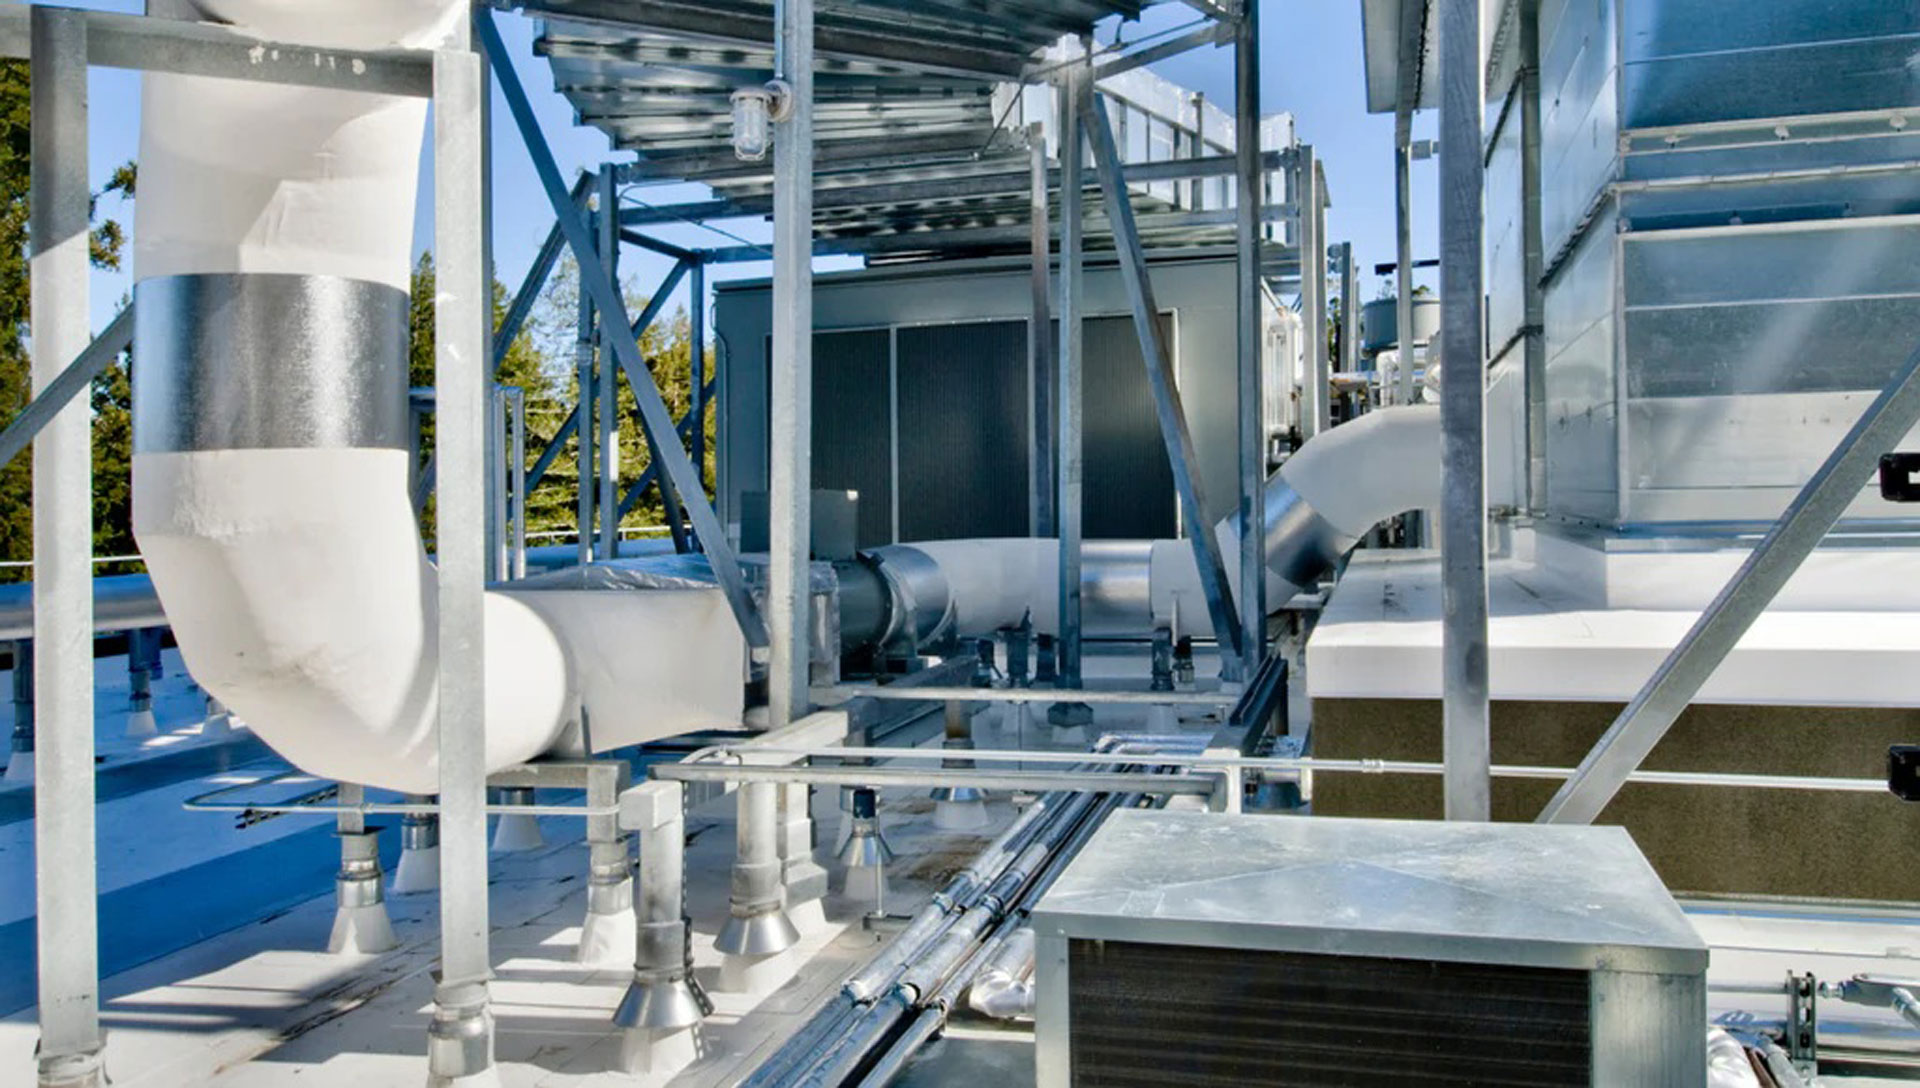
In addition to design and manufacturing, we also offer full-service solutions, including installation, validation, and ongoing servicing. Our expert team works closely with clients to ensure seamless implementation and optimal long-term performance. By providing end-to-end support, we ensure that our solutions continue to meet evolving industry standards and client requirements, enhancing both productivity and operational efficiency.
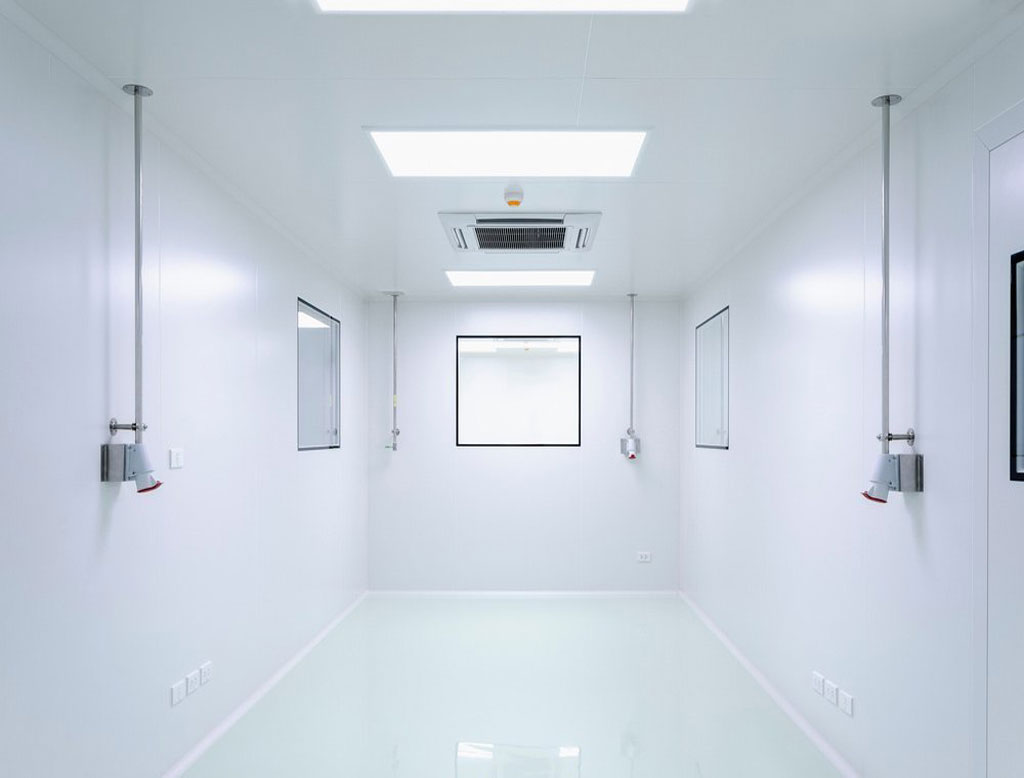
Read MoreWe deliver end-to-end clean room project solutions, encompassing engineering, in-house manufacturing, installation, and validation in full compliance with ISO, GMP, and regulatory standards. Our clean rooms are engineered to provide precise control over airborne particles, temperature, humidity, pressure differentials, and airflow patterns. All critical clean room components—including modular wall and ceiling panels, clean room doors, HVAC systems, AHUs, and filtration units—are manufactured using advanced fabrication technology and stringent quality control processes. This ensures superior performance, long service life, and seamless system integration. Our technical expertise enables us to design and execute customized clean room environments for pharmaceuticals, biotechnology, medical devices, electronics, and healthcare manufacturing. By combining robust engineering, validated performance, and efficient project execution, we help clients achieve contamination control, operational reliability, and regulatory compliance with confidence.
PKB Projects Pvt. Ltd. is part of a diversified group with a strong presence across multiple industries and is led by a dynamic team of young professionals.
Our team comprises highly skilled and experienced engineers who have worked with reputed HVAC organizations, bringing strong technical expertise and global project experience.
From design to execution and commissioning, we provide end-to-end support with in-house consulting expertise and seamless coordination with external consultants.
Post-commissioning, we ensure smooth handover and provide operational support to help your engineering team fully adapt to the installed systems.
We manufacture modular clean room partitions designed for easy installation, superior hygiene, and durability—ideal for controlled environments.
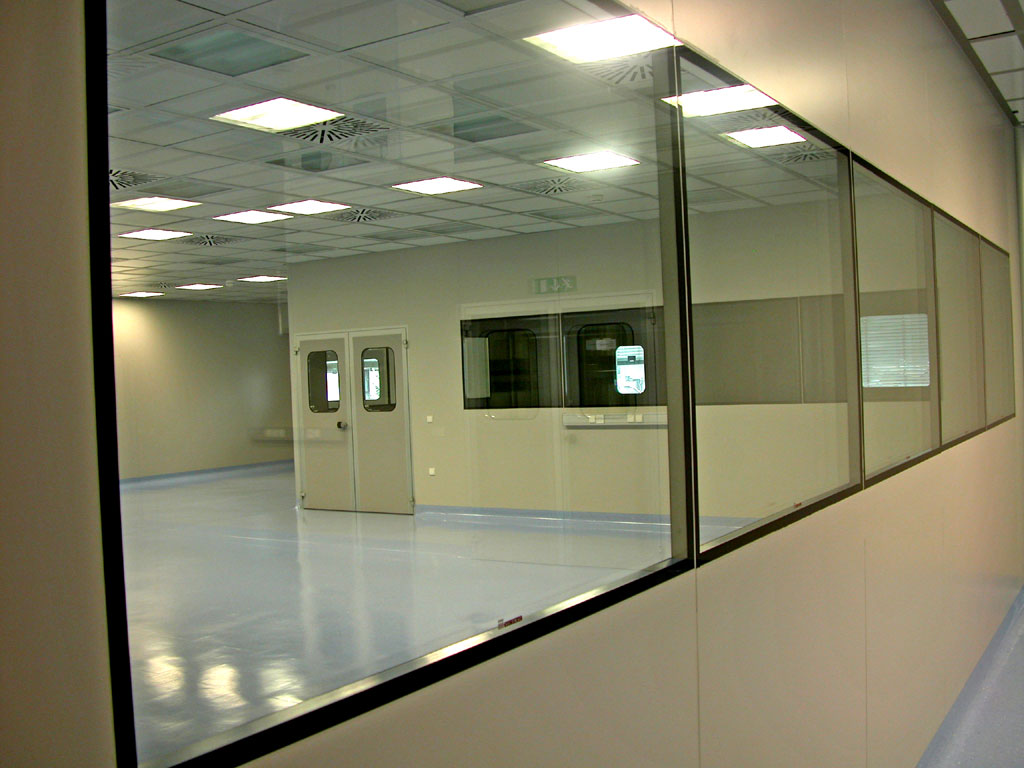
We design clean room flush windows with seamless finishes, double glazing,and easy maintenance—ensuring visibility, hygiene, and airtight performance.
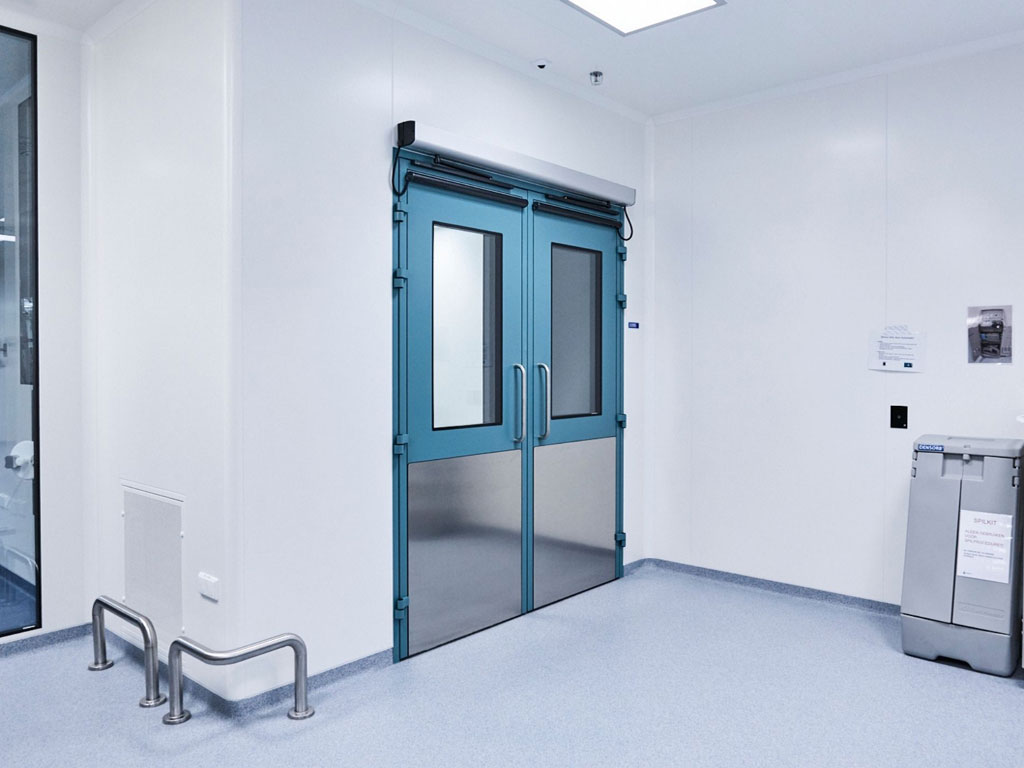
We provide durable fire-rated doors with heat-resistant cores and advanced seals to slow fire spread, protect lives, and meet modern fire safety standards...
PKB Projects provides premium swing doors that combine durability, smooth operation, and modern design. Ideal for residential and commercial spaces, they ensure easy access, security, and lasting performance...
We provide Qualification & Validation services to ensure equipment, systems, and processes meet compliance and deliver reliable, consistent results.
PKB Projects delivers turnkey solutions from design to commissioning, ensuring quality, timely execution, and complete client satisfaction.

We provide high-quality Air Handling Units (AHUs) for efficient air circulation, temperature control, filtration, and indoor air quality.
We provide precision chiller and boiler piping solutions for efficient, reliable, leak-proof, and energy-efficient industrial performance.
PKB Projects provides HEPA filter terminal boxes for cleanrooms, ensuring ultra-clean airflow, high filtration, and contamination control.